How do you find a workshop’s real bottleneck?
A workshop bottleneck is the stage that limits completed work for a defined flow. Follow representative jobs, compare usable capacity and protect the constrained stage from avoidable delays or missing information. Test changes against good output and customer demand before investing in equipment that may simply move the queue elsewhere.
Keep these in mind
- The busiest person or machine is not necessarily the constraint.
- Protect scarce capacity from avoidable waiting and rework.
- Recheck the whole process after an improvement moves the bottleneck.
Trace completed work through the shop
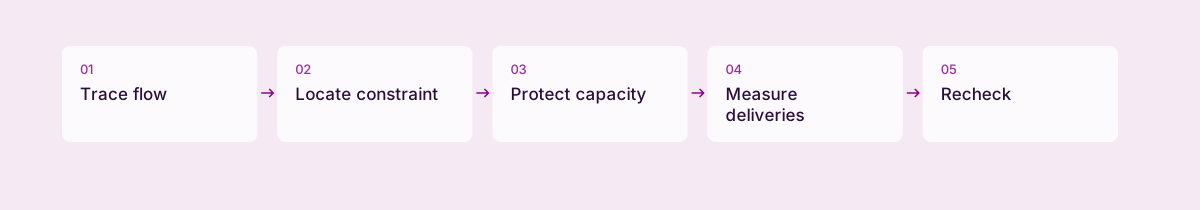
The Theory of Constraints, developed by Eliyahu Goldratt, directs attention to the factor limiting the system’s goal. Goldratt Research Labs describes five focusing steps: identify, exploit, subordinate, elevate and repeat. For a workshop, translate the goal into good jobs delivered to customers.
Draw the route for your main job family: specification, cutting, fabrication, finishing, inspection and dispatch. Count what waits before each stage and ask why. A busy cutter can coexist with an idle finishing station.
The wrong jobs may have been cut, or a required drawing may be missing.
Observe several days, including an ordinary day and a difficult one. A single machine breakdown is important, but it may not identify the normal constraint.
An illustrative five-person workshop
Imagine a metal workshop with two people cutting and preparing parts. It also has one certified welder, one finisher and an owner handling sales and purchasing. The team can prepare 12 standard assemblies daily, weld six and finish eight.
There is demand for nine good assemblies. Welding is the first capacity hypothesis.
Before hiring, watch the welder’s working day. Time spent finding drawings, sorting incorrect parts or answering routine progress questions consumes the very capacity that appears scarce. Moving those avoidable tasks may release useful hours.
Do not remove necessary rest, safety practices or inspection.
| Stage | Potential daily output | Question to investigate |
|---|---|---|
| Preparation | 12 | Are the right kits ready? |
| Welding | 6 | What interrupts skilled work? |
| Finishing | 8 | Can it absorb a welding improvement? |
Protect the constraint without creating a mountain
Prepare a small, agreed buffer of ready work before the scarce stage. A ready kit includes correct parts, approved dimensions and a named priority. A pile of half-prepared jobs does not offer the same protection.
The ACCA discussion of throughput and constraints explains why decisions should consider the whole system. Producing extra parts upstream can increase stock without increasing deliveries.
If better preparation raises welding capacity above finishing capacity, review finishing next. If demand is below available capacity, winning suitable orders may become the main constraint. The method should change your next decision, not become a permanent label attached to one employee.
A practical first-week trial
Select one improvement that the team can reverse. For example, the owner approves a complete job pack the previous afternoon. Someone else answers routine status questions during a protected fabrication period.
- List the last ten late jobs and the stage where each first became blocked.
- Observe the suspected constraint and classify avoidable lost time.
- Prepare one day of correctly specified work before that stage.
- Control upstream release so more jobs do not enter than downstream stages can absorb.
- Compare good deliveries, waiting time and overtime after the trial.
Decide when investment is justified
Additional equipment or training is easier to judge when you know what it would release. Estimate extra good output, demand for that output, ongoing costs and downstream needs. A faster machine may also require more power, handling, maintenance or inspection.
Keep a decision note showing the original assumption, trial period and actual result. For a delayed order, record the constrained stage, responsible person and next check. Confirm completion at that stage before moving the job forward.
An investment review should compare good output and customer demand, not just the hours for which a machine was running.
Common questions
How can a workshop identify its constraint?
Follow a representative job and record where it repeatedly waits. Compare that observation with usable capacity and demand. A busy workstation is not necessarily the one limiting completed orders.
When is buying another machine justified?
Estimate the additional good output customers would buy, including staffing, maintenance and downstream capacity. Test a less expensive process change when the delay comes from missing information or poor sequencing.
Sources & further reading
Primary references for the facts and frameworks discussed. Worked examples and recommendations are Daltn’s own analysis.
- Introduction to Theory of Constraints, Goldratt Research Labs ↗
Primary practitioner explanation of the five focusing steps.
- Throughput accounting and constraints, ACCA ↗
Explains system constraints and decision examples.
Published by the team building Daltn. Comparisons are first-party analysis, not independent reviews. Our editorial approach.